The Injection Blow Molding Process produces hollow plastic parts through a two-stage process that starts with injection molding a preform and finishes by inflating that preform into its final shape inside a blow mold. This approach differs from extrusion blow molding, which forms a continuous tube of plastic rather than a discrete injection-molded preform, and the difference in starting point gives this process distinct advantages for certain part types.
This article looks closely at how injection blow molding works, the materials and tooling it requires, and where it fits compared to other blow molding methods. The goal is to help engineers and procurement professionals understand when this specific process is the right choice for a hollow plastic component.
What the Injection Blow Molding Process Is
The Injection Blow Molding Process is a manufacturing process that produces hollow parts, most commonly small precision containers, by first injection molding a preform around a core rod and then transferring that preform to a blow mold where compressed air inflates it into its final shape. The core rod carries the preform between stations, keeping the neck finish and any threaded features accurately formed throughout the process.
Because the preform itself is injection molded, this two-stage process produces parts with more consistent wall thickness and more precise neck geometry than extrusion-based blow molding methods. This precision is the main reason the process is selected over alternatives for applications where dimensional accuracy at the neck or opening matters most.
How the Injection Blow Molding Process Works
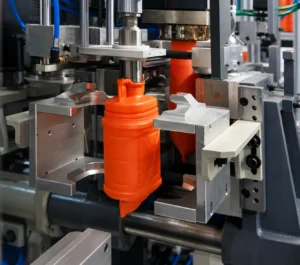
A typical Injection Blow Molding Process cycle moves through three stations built around a rotating or shuttle-type core rod system. At the first station, molten plastic is injected around the core rod to form the preform, similar to a standard injection molding shot but shaped to become the starting point for inflation rather than a finished part.
The core rod then carries the still-warm preform to the second station, where it is enclosed in a blow mold and inflated with compressed air to take the shape of the final part. At the third station, the finished part is ejected from the core rod, which then returns to the first station to begin the cycle again. This continuous, integrated cycle is what distinguishes the process from processes requiring the preform to be reheated in a separate step.
Materials Used in the Injection Blow Molding Process
Polyethylene, polypropylene, and PET are among the most common materials used in the process, selected based on the clarity, chemical resistance, and barrier properties the application requires. PET in particular is widely used for applications where transparency and a precise neck finish are both important, such as small pharmaceutical or cosmetic containers.
Material selection for the Injection Blow Molding Process must account for how the resin behaves during the brief window between preform formation and inflation, since the material needs to retain enough heat and stretch characteristics to inflate cleanly at the second station without cooling too much between steps. This timing sensitivity is one of the process considerations that sets it apart from other blow molding methods.
Precision Advantages for Neck Finish and Wall Thickness
The core rod used throughout the Injection Blow Molding Process maintains precise control over the neck and opening geometry from the first station through ejection, producing dimensional consistency that is difficult to achieve with processes that shape the neck only during a final inflation step. This makes the process well suited to containers with threaded closures, dispensing pumps, or other features that must mate precisely with a cap or fitment.
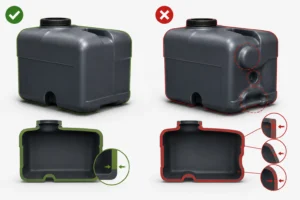
Wall thickness distribution is also generally more uniform with this process than with extrusion blow molding, since the preform is formed under injection molding conditions that allow more direct control over material distribution before inflation even begins. For small, precision containers, this uniformity translates into more consistent performance and appearance across a production run.
Tooling and Core Rod Considerations
Tooling for the Injection Blow Molding Process includes the injection mold that forms the preform, the blow mold that shapes the final part, and the core rods that carry the part between stations, all of which must be dimensionally coordinated to work together through the full cycle. Core rod design is particularly important, since any inconsistency in the rods used across multiple cavities can introduce part-to-part variation.
Because this tooling is more complex than single-mold processes, the upfront investment is generally higher, making the process better suited to programs with production volumes that justify the multi-station setup. Suppliers experienced in injection blow molding can help evaluate whether a program’s expected volume supports this investment.
Injection Blow Molding Process Compared to Extrusion Blow Molding
Extrusion blow molding forms a continuous parison of plastic that is captured and inflated between two mold halves, an approach well suited to larger parts and parts with more complex, asymmetric shapes such as handles or offset necks. The Injection Blow Molding Process is generally better suited to smaller, more precise containers where neck accuracy and wall thickness consistency matter more than overall part size or shape complexity.
Choosing between the two processes typically comes down to part size, required precision, and production volume, and some parts are simply not practical to produce with injection blow molding due to size or geometry constraints that favor the extrusion approach instead. A knowledgeable supplier should be able to recommend the appropriate process based on the specific part rather than defaulting to whichever process they happen to run.
Applications Across Industries
Pharmaceutical and nutraceutical packaging represents one of the largest application areas for the Injection Blow Molding Process, where precise neck finishes for child-resistant closures and dropper fitments are essential. Cosmetic and personal care containers also rely heavily on the process for small bottles requiring precise pump or spray fitment.
Food and beverage applications use injection blow molding for small single-serve containers, while medical and laboratory applications use the process for specimen containers and other small vessels requiring consistent, precise geometry. Across these industries, the common requirement is a small container where neck precision matters more than overall part volume.
Quality Control and Dimensional Consistency
Because the core rod carries the part through every station of the cycle, dimensional inspection typically focuses on neck finish accuracy, wall thickness distribution, and any variation introduced by differences between individual core rods across a multi-cavity tool. First article inspection should verify these dimensions against drawing tolerances before a program moves into full production.
Ongoing process monitoring tracks cycle time consistency, mold temperature, and air pressure during inflation, since drift in any of these parameters can affect wall thickness or introduce cosmetic defects even when overall part dimensions remain within tolerance. Suppliers with mature programs document these parameters as part of their standard production record. The FDA’s guidance on process validation provides broader context on maintaining documented and controlled manufacturing processes for regulated applications.
Why Hi-Rel Plastics Supports Injection Blow Molding Programs
Hi-Rel Plastics & Molding evaluates the Injection Blow Molding Process alongside its other molding capabilities to help customers select the right process for their specific container requirements. The company’s engineering team reviews part geometry, neck finish requirements, and production volume before recommending injection blow molding or an alternative process.
Hi-Rel’s ability to support both injection blow molding and other molding processes under one quality system gives customers a single point of contact for evaluating tradeoffs between processes rather than receiving a recommendation biased toward whichever equipment a supplier happens to own. That objectivity is valuable during the earliest stages of a new container program.
Ready to Explore the Injection Blow Molding Process for Your Program?
The Injection Blow Molding Process offers precision advantages for small containers with demanding neck finish and wall thickness requirements, but it is not the right process for every hollow part. Evaluating part size, geometry, and expected volume early helps determine whether injection blow molding or an alternative process will deliver the best result.
Hi-Rel Plastics & Molding welcomes inquiries from engineers and procurement professionals evaluating the Injection Blow Molding Process for an upcoming container program. Contact Hi-Rel Plastics & Molding to share your part requirements and discuss how Hi-Rel’s capabilities can support your project.